Leave Your Message
Featured alkaline chemistry engineered specifically for heavy-duty scale removal, alkalinity enhancement, and industrial process stability.
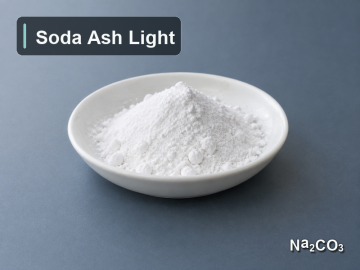
Fast-dissolving grade suited for chemical softening, non-carbonate scale elimination, and calcium conversion in primary water systems.
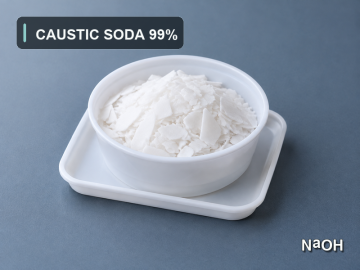
Ultra-pure 99% flake/pearl caustic soda designed to dissolve complex silicate encrustations, organic build-ups, and neutralize acidic wash waters.
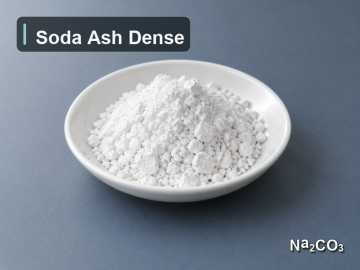
High-density granular media minimizing dusting in automated silos, tailored for constant feed systems in large-scale cooling circuits.
High-performance sodium hydroxide flakes engineered specifically for chemical boil-outs, silica scaling dissociation, and high-temp cleaning loops.
Understanding the thermodynamic and chemical behaviors of sodium hydroxide (NaOH) when attacking recalcitrant mineral and organic scales.
Silica ($SiO_2$) scales represent the most obstinate thermal barriers in boiler feedwaters and cooling towers. Unlike carbonate scales soluble in mineral acids, polymerized silica forms vitreous, glass-like layers. Caustic soda converts non-reactive amorphous silica into soluble sodium silicates ($Na_2SiO_3$) through elevated hydroxyl-ion activity at pH thresholds above 11.5, allowing efficient flush-out without metallurgy loss.
Calcium sulfate ($CaSO_4$ / gypsum) deposits resist direct acidic removal. Industrial descaling protocols deploy concentrated caustic soda solutions (often co-formulated with soda ash or organic chelators) to drive phase transformation from gypsum into acid-soluble calcium carbonate or softer, friable hydrous complexes that can be purged rapidly using minimal acid rinsing cycles.
Industrial scale rarely exists as purely crystalline minerals; it is heavily bound by a sticky, polymeric extracellular matrix (EPS) from biofouling and hydrocarbon trace oils. Caustic soda rapidly hydrolyzes fats, saponifies fatty acids, and disperses biological binders, fragmenting scale lattices and exposing embedded mineral foundations for comprehensive chemical stripping.
How global resource circularity and industrial zero liquid discharge (ZLD) architectures drive caustic soda adoption.
The industrial water treatment landscape is navigating massive transformation driven by stringent Zero Liquid Discharge (ZLD) regulations and water scarcity. Facilities in thermoelectric generation, petroleum refining, chemical synthesis, and mining can no longer rely on routine blowdown and water replenishment. Instead, concentration factors inside cooling loops and brine concentrators are driven to thermodynamic saturation limits, accelerating catastrophic scale accumulation.
In this context, Caustic Soda (Sodium Hydroxide) serves as the fundamental backbone chemical across both preventative and corrective water treatment matrices:
Emerging data indicates global industrial demand for water-grade caustic soda will outpace standard chemical GDP growth rates, expanding at a CAGR of 4.8% through 2032. The primary driver is not merely volumetric throughput, but the demand for strict assay consistency: low iron, minimal chloride contamination, and uniform carbonate boundaries.
When selecting a chemical supply partner for high-consequence descaling operations, industrial operators require supply chain reliability to eliminate catastrophic unplanned plant downtime. RMG meets these strict supply-chain tolerances with comprehensive logistics controls and deep manufacturing integrations.
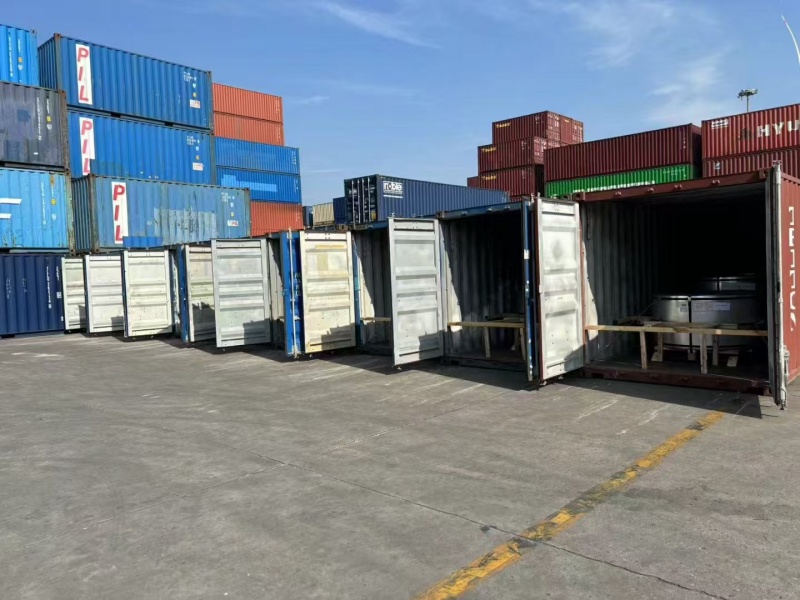
RIVER AND MOUNTAIN GLOBAL LIMITED, also known as RMG, is a global chemical products supplier with more than 20 years of experience in the chemical industry.
We specialize in the export of chemical products used in glassware, printing and dyeing, water treatment, detergents, food and feed additives, fertilizers, desiccants, plastics, minerals, paper-making, and foaming agents.
With deep industry knowledge, reliable supplier resources, and a strong understanding of international markets, RMG helps global buyers solve key sourcing challenges: stable quality, competitive pricing, reliable supply, and efficient service.
Our products are sourced from national-level enterprises and trusted manufacturers, ensuring consistent product quality and long-term supply stability for customers worldwide.
At RMG, we focus on what matters most to chemical product buyers:
Competitive Price
We help customers control purchasing costs through strong sourcing capability and long-term supplier cooperation.
Reliable Product Source
Our supply network is built on qualified manufacturers with stable production capacity and quality assurance.
Stable Quality
We select products from reputable enterprises to reduce quality risk and support repeat purchasing.
Professional Service
From inquiry to shipment, our team responds quickly and supports customers with practical export experience.
Global Market Experience
With business covering 50+ countries and regions, we understand the needs of buyers across Asia-Pacific, Europe, North America, Latin America, the Middle East, Africa, and Oceania.
Our vision is to become a trusted long-term chemical supply partner for global buyers.
We believe that chemical trade is not only about price, but also about stability, responsibility, and trust. RMG is committed to building sustainable partnerships with customers who value consistent quality, reliable supply, and professional cooperation.
We aim to support customers in reducing sourcing risks, improving procurement efficiency, and gaining stronger competitiveness in their local markets.
Experience in the chemical industry
Global business coverage
Serving industries including water treatment, detergents, fertilizers, food and feed additives, paper-making, plastics, and more
Products sourced from national-level enterprises and reliable manufacturers
RMG was founded with a clear purpose: to make chemical product sourcing more reliable, more efficient, and more valuable for international buyers.
Over the past 20 years, we have witnessed the changing demands of the global chemical market. Buyers need more than a product list; they need a partner who understands market fluctuations, supply risks, documentation requirements, and long-term cooperation.
That is why RMG continues to focus on three core values: competitive pricing, dependable supply, and customer satisfaction. These values guide every quotation, every shipment, and every partnership we build.
Today, RMG continues to grow with customers around the world, providing chemical products and sourcing support across multiple industries and markets.
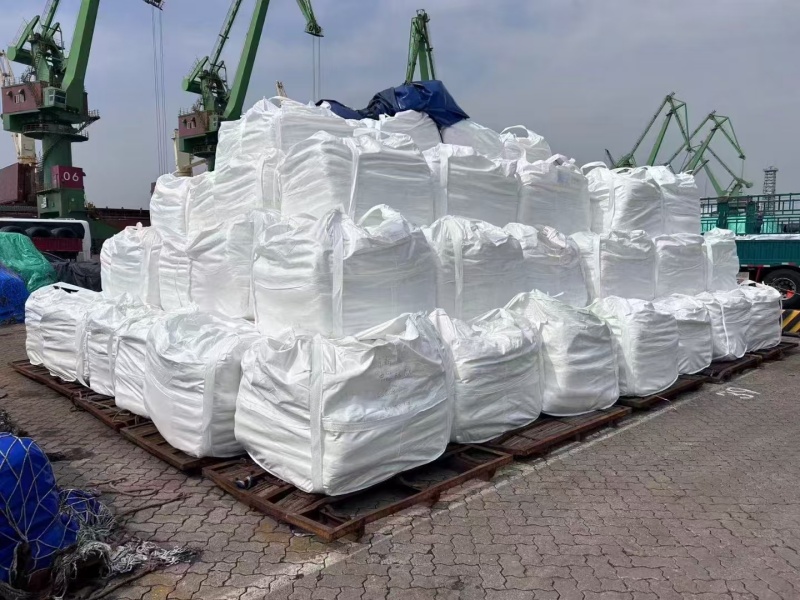
RMG serves customers in more than 50 countries and regions, with comprehensive business coverage across major world markets.
Our wide market coverage allows us to respond to different purchasing needs, regional standards, and application requirements with greater flexibility.
RMG works closely with reliable chemical manufacturers and national-level enterprises to ensure product stability and supply continuity.
For global buyers, this means more than finding a supplier. It means working with a sourcing partner who can provide quality consistency, supply reliability, and long-term cooperation value.
Explore our specialized portfolio of sodium hydroxide and alkaline process compounds optimized for high-efficiency plant operations.
Spherical micro-pearls offering fast dissolution characteristics, minimal dusting, and precise dosing for automated membrane CIP systems.
Heavy-grade industrial flakes engineered for power utility boiler chemical flushes and deep dissolution of recalcitrant silicate scales.
High-solubility sodium carbonate for hardness precipitation, calcium removal, and neutralizing raw boiler feedwater feeds.
High-bulk density granular compound, formulated to prevent bridging in bulk industrial feed bins and cooling tower chemical loops.
Low-chloride, high-alkalinity reagent tailored specifically for regeneration of strong-base anion resins and silica stripping.
Rapid dispersion chemical buffer engineered to neutralize post-acid-descaling wastewater streams before environmental discharge.
Heavy-density sodium carbonate used to convert recalcitrant heavy metal sulfates into manageable insoluble carbonate sludges.
Thermal-stable alkaline chemical agent designed to eliminate complex multi-mineral incrustations across continuous black-liquor and brine evaporators.