Leave Your Message
A comprehensive analysis of Calcium Chloride and Magnesium salts in continuous dyeing, printing paste rheology, and sustainable industrial operations.
Cellulosic substrates inherently acquire an electronegative surface charge in aqueous baths. Divalent ions such as Ca²⁺ and Mg²⁺ exert double the screening efficiency of conventional sodium ions, compressing the electrical double layer and accelerating dye fixation without hyper-saline effluent stress.
In high-definition textile printing formulations, magnesium salts act as mild, latent acid-releasing catalysts during heat steaming. This mechanism ensures impeccable fixation for reactive dyes and pigment binders without premature batch coagulation or viscosity destabilization.
Modern textile mills are shifting from massive monovalent salt dosages (Glauber's salt or NaCl) to precision divalent salts like Calcium Chloride and Magnesium Chloride, drastically reducing total dissolved solids (TDS) and lowering freshwater consumption in reverse osmosis effluent plants.
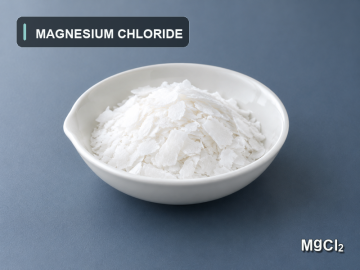
The global textile coloration sector is encountering historic transformations driven by stringent wastewater standards, water stewardship mandates, and the shift toward digital high-speed reactive printing. Within this dynamic landscape, the application of alkaline earth mineral salts—principally Calcium Chloride (CaCl₂) and Magnesium compounds (Magnesium Chloride, MgCl₂, and Magnesium Sulfate, MgSO₄)—has elevated far beyond rudimentary textile auxiliaries into essential process enhancers.
During the dyeing of natural fibers like cotton, viscose, and linen, cellulose surfaces undergo ionization in water, generating a negative zeta potential. This electrostatic repulsion naturally deters anionic chromophores present in reactive, vat, and direct dyes. Traditionally, colossal quantities of sodium chloride or sodium sulfate (often up to 60-100 g/L) were injected into dye liquors to force exhaust. However, according to the Schulze-Hardy rule, the critical coagulation and ionic compression concentration is inversely proportional to the sixth power of ion valency. By leveraging divalent Calcium (Ca²⁺) and Magnesium (Mg²⁺) cations, textile engineers can compress the electrical double layer with significantly reduced salt volumes, leading to high dye exhaustion, deep shade yields, and dramatically reduced chemical cargo costs.
In textile screen and digital ink printing, reactive paste formulations demand absolute rheological stability at ambient temperatures paired with swift cross-linking kinetics under high-temperature superheated steaming. Magnesium chloride serves as an indispensable latent catalyst in pigment and reactive dye printing pastes. At room temperature, it maintains stable pH conditions, precluding premature hydrolysis of reactive monochlorotriazine or vinyl sulfone dye systems. Once entering the steamer (102°C–165°C), controlled dissociation releases micro-acidic equivalents, speeding fiber-dye etherification and urethane binder condensation without fiber embrittlement.
The worldwide market for textile printing and dyeing chemicals continues to shift toward sustainable manufacturing hubs in Southeast Asia, South Asia, and the Mediterranean basin. As Zero Discharge of Hazardous Chemicals (ZDHC) frameworks enforce rigorous Total Dissolved Solids (TDS) and biological toxicity thresholds, traditional heavy salt loading is rapidly falling out of favor. Industrial facilities are adopting engineered blends of Calcium Chloride and Magnesium Chloride to optimize osmotic pressure in dye baths, decrease rinse cycle volumes, and lower power requirements for membrane biological reactors (MBR) and zero-liquid-discharge (ZLD) evaporators.
RIVER AND MOUNTAIN GLOBAL LIMITED, also known as RMG, is a global chemical products supplier with more than 20 years of experience in the chemical industry.
We specialize in the export of chemical products used in glassware, printing and dyeing, water treatment, detergents, food and feed additives, fertilizers, desiccants, plastics, minerals, paper-making, and foaming agents.
With deep industry knowledge, reliable supplier resources, and a strong understanding of international markets, RMG helps global buyers solve key sourcing challenges: stable quality, competitive pricing, reliable supply, and efficient service.
Our products are sourced from national-level enterprises and trusted manufacturers, ensuring consistent product quality and long-term supply stability for customers worldwide.
At RMG, we focus on what matters most to chemical product buyers:
Competitive Price
We help customers control purchasing costs through strong sourcing capability and long-term supplier cooperation.
Reliable Product Source
Our supply network is built on qualified manufacturers with stable production capacity and quality assurance.
Stable Quality
We select products from reputable enterprises to reduce quality risk and support repeat purchasing.
Professional Service
From inquiry to shipment, our team responds quickly and supports customers with practical export experience.
Global Market Experience
With business covering 50+ countries and regions, we understand the needs of buyers across Asia-Pacific, Europe, North America, Latin America, the Middle East, Africa, and Oceania.
Our vision is to become a trusted long-term chemical supply partner for global buyers.
We believe that chemical trade is not only about price, but also about stability, responsibility, and trust. RMG is committed to building sustainable partnerships with customers who value consistent quality, reliable supply, and professional cooperation.
We aim to support customers in reducing sourcing risks, improving procurement efficiency, and gaining stronger competitiveness in their local markets.
Experience in the chemical industry
Global business coverage
Serving industries including water treatment, detergents, fertilizers, food and feed additives, paper-making, plastics, and more
Products sourced from national-level enterprises and reliable manufacturers
RMG was founded with a clear purpose: to make chemical product sourcing more reliable, more efficient, and more valuable for international buyers.
Over the past 20 years, we have witnessed the changing demands of the global chemical market. Buyers need more than a product list; they need a partner who understands market fluctuations, supply risks, documentation requirements, and long-term cooperation.
That is why RMG continues to focus on three core values: competitive pricing, dependable supply, and customer satisfaction. These values guide every quotation, every shipment, and every partnership we build.
Today, RMG continues to grow with customers around the world, providing chemical products and sourcing support across multiple industries and markets.
RMG serves customers in more than 50 countries and regions, with business coverage across global chemical corridors.
Our wide market coverage allows us to respond to different purchasing needs, regional standards, and application requirements with greater flexibility.
RMG works closely with reliable chemical manufacturers and national-level enterprises to ensure product stability and supply continuity.
For global buyers, this means more than finding a supplier. It means working with a sourcing partner who can provide quality consistency, supply reliability, and long-term cooperation value.