Leave Your Message
Engineered raw materials driving high-performance synthesis, acidity control, and moisture barrier formulations across modern manufacturing environments.
Bridging the critical gap between passive sorption kinetics and chemical thermodynamic stability in heavy-duty industrial desiccant packaging.
Industrial packaging faces an unrelenting adversary: cyclic condensation, microclimatic relative humidity (RH) spikes, and chemical cross-reactivity during transcontinental maritime and multimodal transit. Acetic Acid Magnesium—chemically recognized as magnesium acetate [Mg(CH₃COO)₂], commonly formulated as a tetrahydrate—occupies a distinct and increasingly vital role in advanced desiccant technology.
Unlike conventional physical adsorbents such as standard amorphous silica gel or activated montmorillonite clay, magnesium acetate introduces dual-action protective properties. It possesses profound deliquescence buffering capacities and specific coordination chemistry that enables structural moisture binding within solid matrices, immobilizing free aqueous vapors without leaking corrosive brines.
By modulating the pH environment inside hermetically sealed containers, Acetic Acid Magnesium also prevents acid-catalyzed oxidative decomposition of moisture-sensitive goods, making it a critical specialty ingredient for premium protective packaging systems.
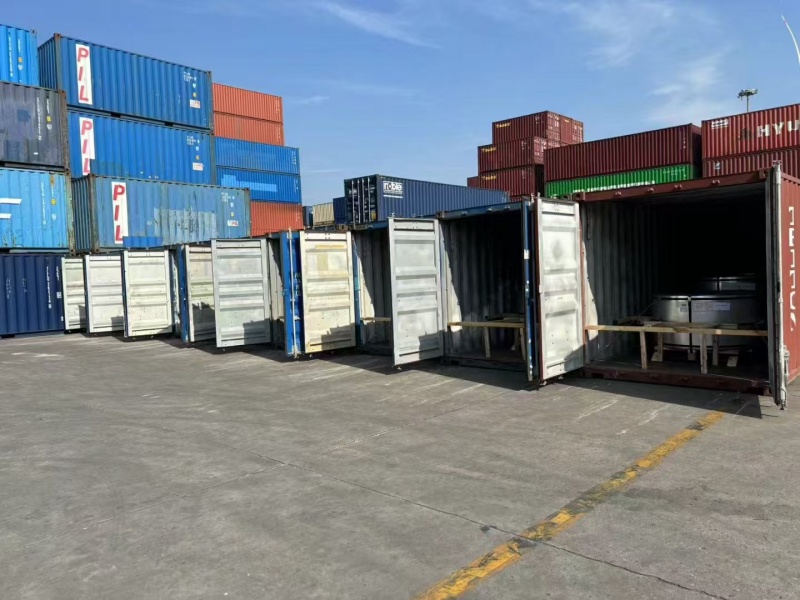
Magnesium acetate operates via progressive stoichiometric hydrate formation. It absorbs moisture by integrating water molecules directly into its crystalline coordinate sphere, preventing liquid phase pooling and maintaining the mechanical integrity of surrounding barrier sachets.
During prolonged industrial storage, packaging polymeric films and adhesives often outgas trace volatile organic acids. Acetic Acid Magnesium compounds act as sacrificial buffering matrices, stabilizing internal atmospheric acidity and thwarting secondary surface corrosion on metallic parts.
With international supply chains shifting away from environmentally aggressive metal halides and cobalt-doped indicators, magnesium acetate salts deliver an inherently non-toxic, biodegradable, and non-halogenated profile that adheres fully to modern global RoHS and REACH mandates.
How global supply chain volatility and technological advances are driving the adoption of modified magnesium-acetate-infused desiccants across precision industries.
1. Aerospace & Precision Electronics Containment: Critical aerospace assemblies, multi-layer printed circuit boards (PCBs), and optoelectronic sensors are acutely prone to micro-corrosion caused by corrosive chloride-based desiccant salts. Acetic Acid Magnesium is integrated into non-dusting polymer fiber pouches, offering rapid dehumidification without introducing airborne ionic halides that degrade gold wire bonding or sensitive solder interfaces.
2. High-Value Pharmaceutical & Diagnostic Kits: Diagnostic reagents and powdered active pharmaceutical ingredients (APIs) require stable low-humidity micro-climates without severe dessication that could strip crystal-bound structural water. Magnesium acetate systems are deployed as RH "buffers," moderating moisture levels within strict thermodynamic envelopes (typically 20% to 40% RH) to preserve bioactive shelf life.
3. Automotive Lithium-Ion Battery Module Transport: The rapid surge in global electric vehicle (EV) component logistics demands desiccants that prevent hydrogen gas evolution and lithium oxidation. Standard moisture traps can fail when exposed to thermal variations. Formulated magnesium acetate matrices provide high thermal threshold retention, ensuring packaging integrity even inside unconditioned cargo holds experiencing extreme heat spikes.
4. Heavy Industrial Machinery & Ocean Freight Shipping: During ocean shipping, containers undergo massive temperature swings resulting in "container rain." Acetic Acid Magnesium blends, incorporated into high-capacity hanging desiccant poles and dry bags, absorb multiple times their weight in water vapor without leaking fluid, safeguarding structural raw steel and heavy machinery from catastrophic pitting.
| Performance Parameter | Magnesium Acetate Compound System | Standard Calcium Chloride (CaCl₂) | Traditional Silica Gel |
|---|---|---|---|
| Corrosion Risk Profile | Negligible (Halide-free, buffer-active) | High (Severe chloride vapor pitting risk) | Inert (No direct corrosion) |
| Deliquescence Leakage | Minimal (Hydrate lattice crystallization) | High (Forms liquid brine requiring complex membranes) | Zero (Adsorptive pore retention) |
| Thermal Stability Envelope | Superior up to elevated shipping temps | Unstable liquid phase transition | Rapid thermal desorption above 50°C |
| Environmental Disposal | Eco-compatible, readily biodegradable organic salt | Halide runoff restrictions in specific jurisdictions | Non-biodegradable synthetic mineral |
RIVER AND MOUNTAIN GLOBAL LIMITED, also known as RMG, is a global chemical products supplier with more than 20 years of experience in the chemical industry.
We specialize in the export of chemical products used in glassware, printing and dyeing, water treatment, detergents, food and feed additives, fertilizers, desiccants, plastics, minerals, paper-making, and foaming agents.
With deep industry knowledge, reliable supplier resources, and a strong understanding of international markets, RMG helps global buyers solve key sourcing challenges: stable quality, competitive pricing, reliable supply, and efficient service.
Our products are sourced from national-level enterprises and trusted manufacturers, ensuring consistent product quality and long-term supply stability for customers worldwide.
At RMG, we focus on what matters most to chemical product buyers:
Competitive Price
We help customers control purchasing costs through strong sourcing capability and long-term supplier cooperation.
Reliable Product Source
Our supply network is built on qualified manufacturers with stable production capacity and quality assurance.
Stable Quality
We select products from reputable enterprises to reduce quality risk and support repeat purchasing.
Professional Service
From inquiry to shipment, our team responds quickly and supports customers with practical export experience.
Global Market Experience
With business covering 50+ countries and regions, we understand the needs of buyers across Asia-Pacific, Europe, North America, Latin America, the Middle East, Africa, and Oceania.
Our vision is to become a trusted long-term chemical supply partner for global buyers.
We believe that chemical trade is not only about price, but also about stability, responsibility, and trust. RMG is committed to building sustainable partnerships with customers who value consistent quality, reliable supply, and professional cooperation.
We aim to support customers in reducing sourcing risks, improving procurement efficiency, and gaining stronger competitiveness in their local markets.
Experience in the chemical industry
Global business coverage
Serving industries including water treatment, detergents, fertilizers, food and feed additives, paper-making, plastics, and more
Products sourced from national-level enterprises and reliable manufacturers
RMG was founded with a clear purpose: to make chemical product sourcing more reliable, more efficient, and more valuable for international buyers.
Over the past 20 years, we have witnessed the changing demands of the global chemical market. Buyers need more than a product list; they need a partner who understands market fluctuations, supply risks, documentation requirements, and long-term cooperation.
That is why RMG continues to focus on three core values: competitive pricing, dependable supply, and customer satisfaction. These values guide every quotation, every shipment, and every partnership we build.
Today, RMG continues to grow with customers around the world, providing chemical products and sourcing support across multiple industries and markets.
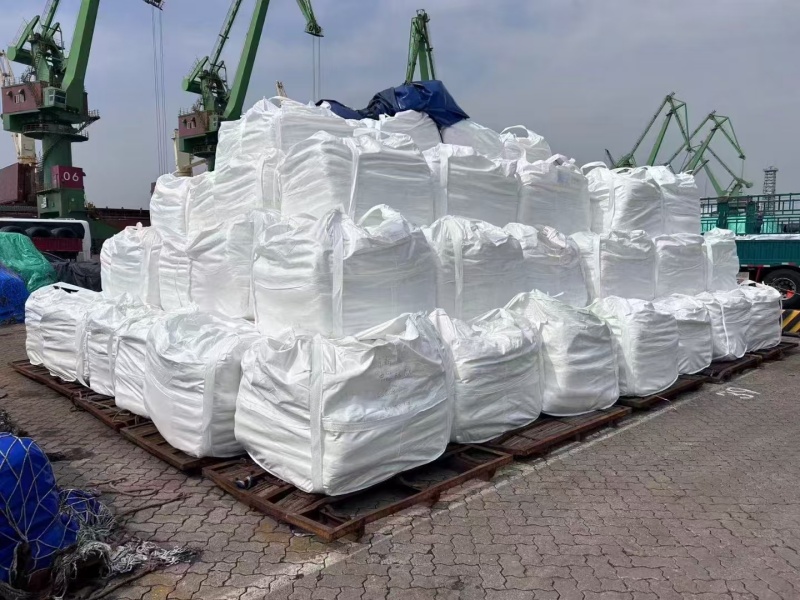
RMG serves customers in more than 50 countries and regions, with business coverage across global industrial centers.
Our wide market coverage allows us to respond to different purchasing needs, regional standards, and application requirements with greater flexibility, facilitating secure chemical packaging, compliant labeling, and predictable delivery windows.
RMG works closely with reliable chemical manufacturers and national-level enterprises to ensure product stability and supply continuity.
For global buyers, this means more than finding a supplier. It means working with a sourcing partner who can provide quality consistency, supply reliability, and long-term cooperation value.
Explore our comprehensive selection of high-grade chemicals tailored for manufacturing, preservation, detergent processing, and industrial applications.